


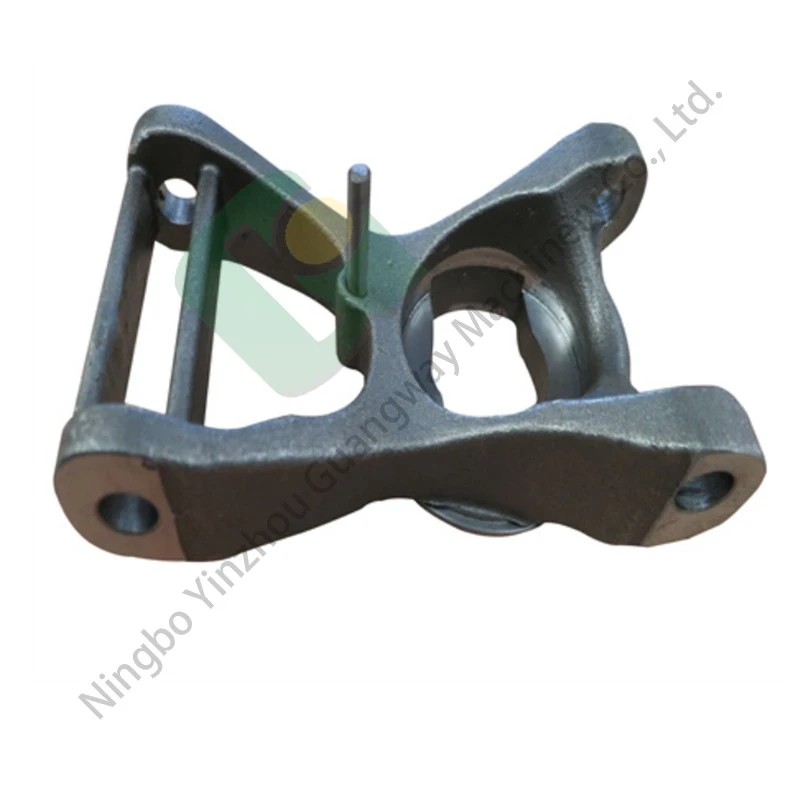


Raw Materials Pre-treatment
- Resin Coating: Pre-coated resins are specifically used. Such resins are selected on heat resistance, on curing, as also on bonding between grains of sand. Some resins which are generally used are phenolic resins, which are also known to form high-strength bonds as also a good surface finish on castings.
Molding Process
- Pattern making: The pattern design is crafted with high precision according to pump casting design. The pattern is constructed from wood, metal, or plastic. The pattern is used in the production of a cavity in a mould made from sand in which molten metal is cast.
- Sand Molding: Pre-coated sand is packed around the pattern in a molding box. The sand is pressed into shape and hardened in order to have a perfect shape and solidity in the mould. The pattern is later removed with care, leaving a cavity in the sand mould with a shape that is similar in shape with that of the pump casting.
- Core making: There are cores that are made in more developed pump structures with pre-coat internal passageways in resin sand. Cores are placed in a mould cavity in an attempt at making internal castings.
Melting And Pouring
- Metal Melting: The appropriate alloy metal that can be pump castings, i.e., cast iron, stainless steel, or bronze, is melted in a furnace. Melting is done with care in a way that it is both in terms of melt temperature as well as in terms of chemical composition.
- Pouring: The metal is cast in a pre-shaped mould made out of sand through a gating arrangement. The gating arrangement is in a design that a free flowing fill in mould cavity is achieved with no flaw in terms of cold shuts as well as porosity.
Cooling And Solidification
- Natural Cooling: The cast is allowed to cool naturally. The rate at which it cools is a consideration because it will impact both its mechanics as well as its microstructure. A rate that is in a controlled rate can assist in attaining its favored toughness, as well as its hardness, ductility.
- Solidification Monitoring: Monitoring is also conducted on solidification temperature distribution in order to determine defects likely to cause cracking as a consequence of nonuniform cooling or hotspots.
Post - Processing
- Shakeout: The cast is shaken out from about the sand once it is hardened sufficiently and cooled in a shakeout operation.
- Finishing Operations: The cast is undergone a series of finishing operations that entail trimming excess metal from gating, surface grinding out rough surfaces, as well as machining in order to achieve the final dimensions as well as surface finishes required in pump components.
- Quality Testing: The castings are inspected once casted with non - destructive means that involve ultrasonic testing, X - ray testing, as well as magnetic particle testing in an effort to determine surface as well as internal defects. They are also dimensionally tested as well as their mechanics in an effort to determine whether they are satisfactory with reference to pump application demands.
Hot Tags: pre-coated resin sand castings for pumps, China pre-coated resin sand castings for pumps manufacturers, suppliers, factory, Pre coated Resin Sand Castings for Heavy Machinery, Pre coated Resin Sand Castings for Machinery, pre coated resin sand castings, Pre coated Resin Sand Castings for Valves, Pre coated Resin Sand Castings for Oil and Gas Industry, Pre coated Resin Sand Castings for Pumps